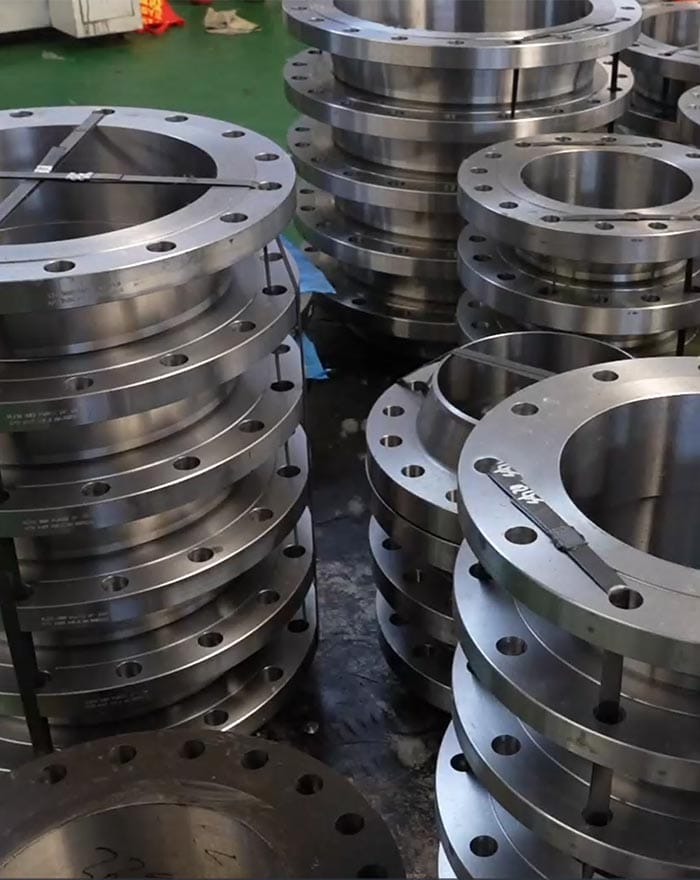
A pipeline coating holiday test locates pinholes, voids, cracks, or other electrical paths through a nonconductive coating to the steel substrate. Wet-sponge and high-voltage methods cover different coating systems and thickness ranges. The approved procedure must define surface condition, grounding, test voltage, electrode, travel rate, marking, repair, and retest.
This guide keeps the scope on 3PE Steel Pipe and the decision promised by the title. It does not replace the governing code, project specification, manufacturer instructions, or an engineering review of the actual service.
Table of Contents
At a Glance
- A holiday is an electrical discontinuity
- Choose the method for coating thickness
- Confirm the substrate can complete the circuit
- Prepare a suitable test surface
- Move the electrode at a controlled rate
- Mark and repair indications traceably
- Avoid damaging sound coating
- Combine holiday testing with other checks
A holiday is an electrical discontinuity
Pinholes, voids, cracks, thin spots, or mechanical damage may expose conductive substrate. Holiday testing locates conductive paths through a nonconductive coating.
It does not by itself measure adhesion or cure. For pipeline coating holiday test, the purpose of this step is to turn “pinholes, voids, cracks, thin spots, or mechanical damage may expose conductive substrate” into a check that can be accepted or rejected. Complete it before 3PE Steel Pipe moves beyond a holiday is an electrical discontinuity, and identify the document or measurement that supports the result.
Choose the method for coating thickness
Wet-sponge and high-voltage methods suit different coating ranges and specifications. The governing coating procedure should define equipment and voltage.
Do not increase voltage simply to find more indications. The practical risk at choose the method for coating thickness is an interface that appears acceptable by itself but fails when assembled. Relate the 3PE Steel Pipe finding to the mating pipe, fitting, structure, instrument, coating, or building element affected by “the governing coating procedure should define equipment and voltage”.
Confirm the substrate can complete the circuit
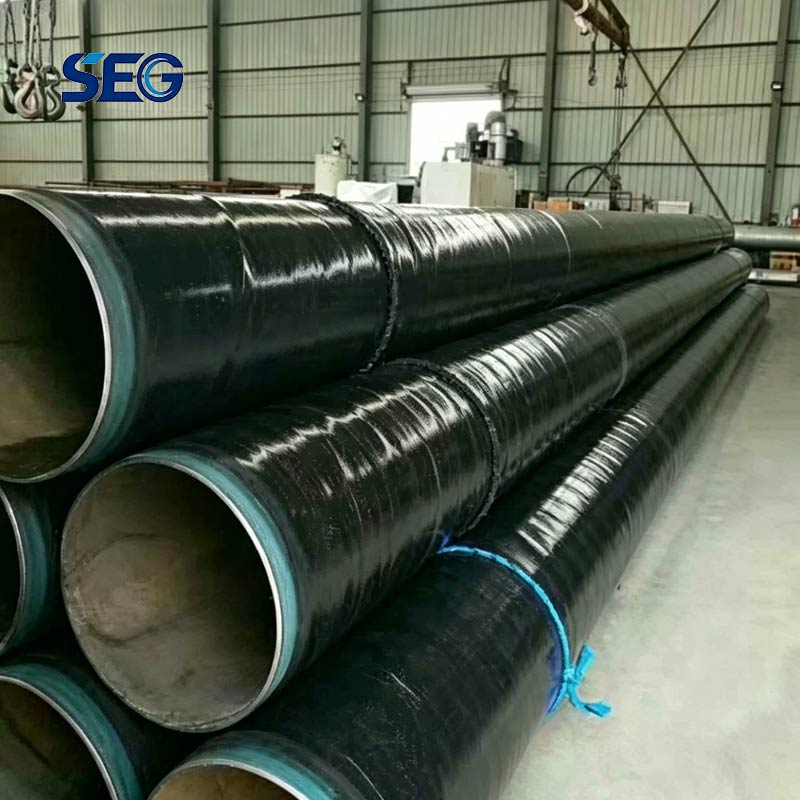
Electrical contact to the steel is essential. Poor grounding can create false confidence.
Verify instrument function on a known standard or test point as the procedure requires. Timing matters here. Evidence for confirm the substrate can complete the circuit is strongest while the relevant marking, surface, dimension, or connection is visible. For pipeline coating holiday test, record the item reference, observed condition, and disposition before later work conceals the feature described by “verify instrument function on a known standard or test point as the procedure requires”.
Prepare a suitable test surface
Coating should be sufficiently cured, reasonably clean, and in the condition required by the method. Surface moisture or contamination can affect indications.
Inspect sharp edges and complex geometry carefully. Keep design and workmanship decisions separate during prepare a suitable test surface. The approved drawing, data sheet, code, or procedure defines the required 3PE Steel Pipe condition; inspection establishes whether the supplied condition meets it. A familiar shop practice cannot replace that comparison.
Move the electrode at a controlled rate
Coverage depends on electrode contact, travel speed, operator technique, and access. Use an electrode suited to pipe diameter and component shape.
Overlap passes so no strip is missed. Review move the electrode at a controlled rate across normal operation, testing, startup, shutdown, and maintenance where those states are relevant. The pipeline coating holiday test decision should remain suitable when temperature, load, flow, access, or support conditions change from the installation state.
Mark and repair indications traceably
Identify defect location before moving on. Repair preparation and material must be compatible with the original system.
Retest the repaired area after the required cure. If mark and repair indications traceably produces a deviation, describe the exact 3PE Steel Pipe condition and affected quantity before proposing repair or use-as-is. Technical approval should address the consequence identified by “repair preparation and material must be compatible with the original system”, not only the commercial or schedule effect.
Avoid damaging sound coating
Excessive test voltage, sharp electrodes, or repeated arcing can create defects. Follow the standard, project specification, and equipment instructions.
Stop if the coating behaves abnormally. Inspection evidence for avoid damaging sound coating should be traceable to the affected 3PE Steel Pipe. Link photographs, reports, gauges, certificates, or drawings to the item or location so that another reviewer can verify why “stop if the coating behaves abnormally” was considered satisfied.
Combine holiday testing with other checks
Thickness, visual condition, adhesion or qualification data, cutbacks, repairs, and handling condition provide different evidence. No single test proves the whole coating system.
Compile results by pipe number or defined lot. Close combine holiday testing with other checks with an explicit status: accepted, rejected, conditionally released, or awaiting information. The final pipeline coating holiday test file should show approved changes and open actions, preventing an unresolved point about “thickness, visual condition, adhesion or qualification data, cutbacks, repairs, and handling condition provide different evidence” from reaching construction or operation.
Standards and Source Documents
Use the edition named by the contract. Primary reference starting points include ISO 21809-1 external coatings, ISO 21809-3 field-joint coatings, AMPP corrosion resources, ASTM standards library. Their scopes differ, so a general reference must not be treated as the acceptance criterion for every product or project.
Related Sirgou Resources
Compare the 3PE Steel Pipe product page with Plastic Coated Steel Pipe and Spiral Steel Pipe. For supplier qualification context, read the pipe and fittings supplier guide. These pages support product research; they do not make adjacent products interchangeable.
Frequently Asked Questions
What should be confirmed first? — pipeline coating holiday test
Pinholes, voids, cracks, thin spots, or mechanical damage may expose conductive substrate. It does not by itself measure adhesion or cure. If the project document is more specific, its requirement controls.
Which interface causes the most mistakes? — pipeline coating holiday test
Electrical contact to the steel is essential. Verify instrument function on a known standard or test point as the procedure requires. If the project document is more specific, its requirement controls.
When should the check be recorded? — pipeline coating holiday test
Identify defect location before moving on. Retest the repaired area after the required cure. If the project document is more specific, its requirement controls.
What belongs in the final acceptance file? — pipeline coating holiday test
Thickness, visual condition, adhesion or qualification data, cutbacks, repairs, and handling condition provide different evidence. Compile results by pipe number or defined lot. If the project document is more specific, its requirement controls.
Before closing a holiday is an electrical discontinuity, connect the requirement “Pinholes, voids, cracks, thin spots, or mechanical damage may expose conductive substrate” with the action “It does not by itself measure adhesion or cure”. In this pipeline coating holiday test review, that connection identifies what was checked, why it matters to 3PE Steel Pipe, and which project record carries the final answer.
Project Takeaway
A pipeline coating holiday test locates pinholes, voids, cracks, or other electrical paths through a nonconductive coating to the steel substrate. Use the article as a decision guide, then put the selected values, acceptance evidence, and approved deviations into the controlled project documents. For product-specific questions, contact Sirgou with the service conditions, size range, quantities, standards, and required documentation.